Guaranteed Production Scalability
Industrial-grade facilities maintain dedicated capacity to fulfill massive seasonal rollouts, recurring team uniform contracts, and large retail inventory restocking effortlessly.
In the global sports apparel and institutional retail markets, efficient supply chain execution, predictable inventory volume, and uncompromised unit economics represent critical pillars of commercial viability. As athletic leagues, fitness franchise networks, corporate merchandising divisions, and retail brands scale their operations, the demand for reliable, high-capacity manufacturing partners intensifies. Navigating high-volume procurement requires an industrial ecosystem capable of maintaining rigorous technical standards across thousands of units without sacrificing structural garment integrity, color consistency, or strict delivery timelines.
As a premier wholesale custom sportswear supplier, Deuka Wears delivers comprehensive bulk manufacturing solutions tailored for athletic distributors, team uniform outfitters, and activewear brands worldwide. By unifying industrial-scale cutting technology, automated sewing lines, stringent quality assurance protocols, and streamlined international logistics under a corporate infrastructure, we empower enterprise clients to optimize their supply chains and maximize operational profitability.
Procuring athletic apparel through fragmented broker networks or multi-tiered distribution channels frequently introduces severe operational vulnerabilities, including inflated cost structures, communication friction, and uncontrollable delivery delays. For organizations managing large-scale inventory rollouts, these supply chain inefficiencies directly impact profit margins and brand reputation.
When you collaborate with an experienced wholesale athletic apparel manufacturer, you secure a direct factory-direct partnership designed to streamline large-scale production while protecting your financial and operational interests.

Optimized Unit Economics (COGS)
Eliminating intermediary middle-men allows enterprise buyers to secure maximum volume discounts, significantly improving profit margins on retail and institutional resale.

Industrial-grade facilities maintain dedicated capacity to fulfill massive seasonal rollouts, recurring team uniform contracts, and large retail inventory restocking effortlessly.

Advanced computerized cutting and standardized assembly lines ensure that every single garment in a 5,000-unit production run matches exact technical specifications.

Coordinated freight forwarding, master carton consolidation, and customs documentation support guarantee predictable, on-time delivery directly to your central distribution hub.
Operating as an established bulk custom sports clothing factory, Deuka Wears maintains absolute oversight across every operational phase of the mass manufacturing lifecycle. Our vertically integrated facility bridges the gap between commercial bulk orders and international retail distribution, ensuring seamless execution for every enterprise client.
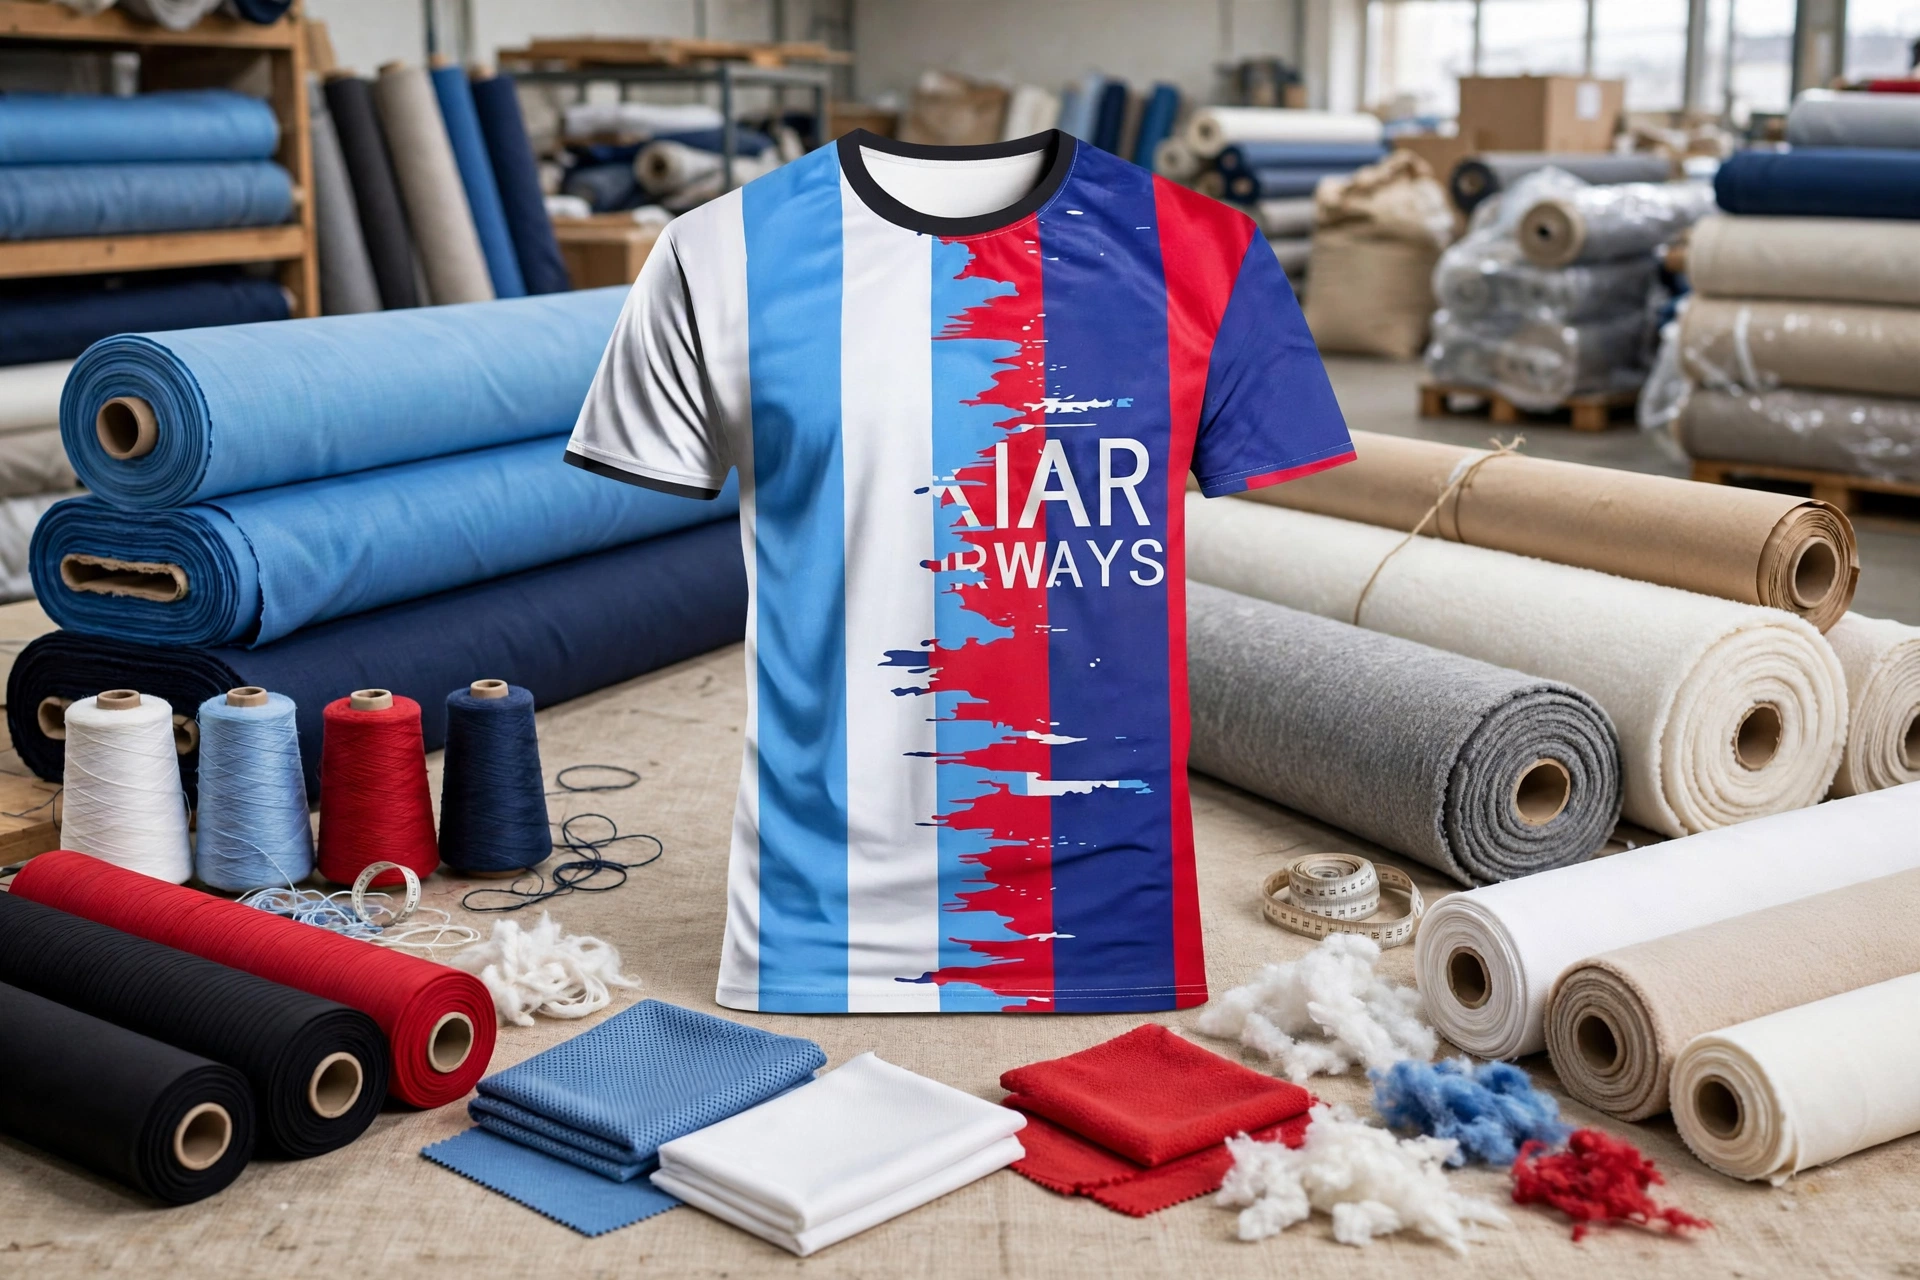
Bulk manufacturing requires consistent, high-volume access to elite technical textiles. We partner directly with leading textile mills to secure premium yarn lots and performance fabrics engineered for demanding athletic environments:
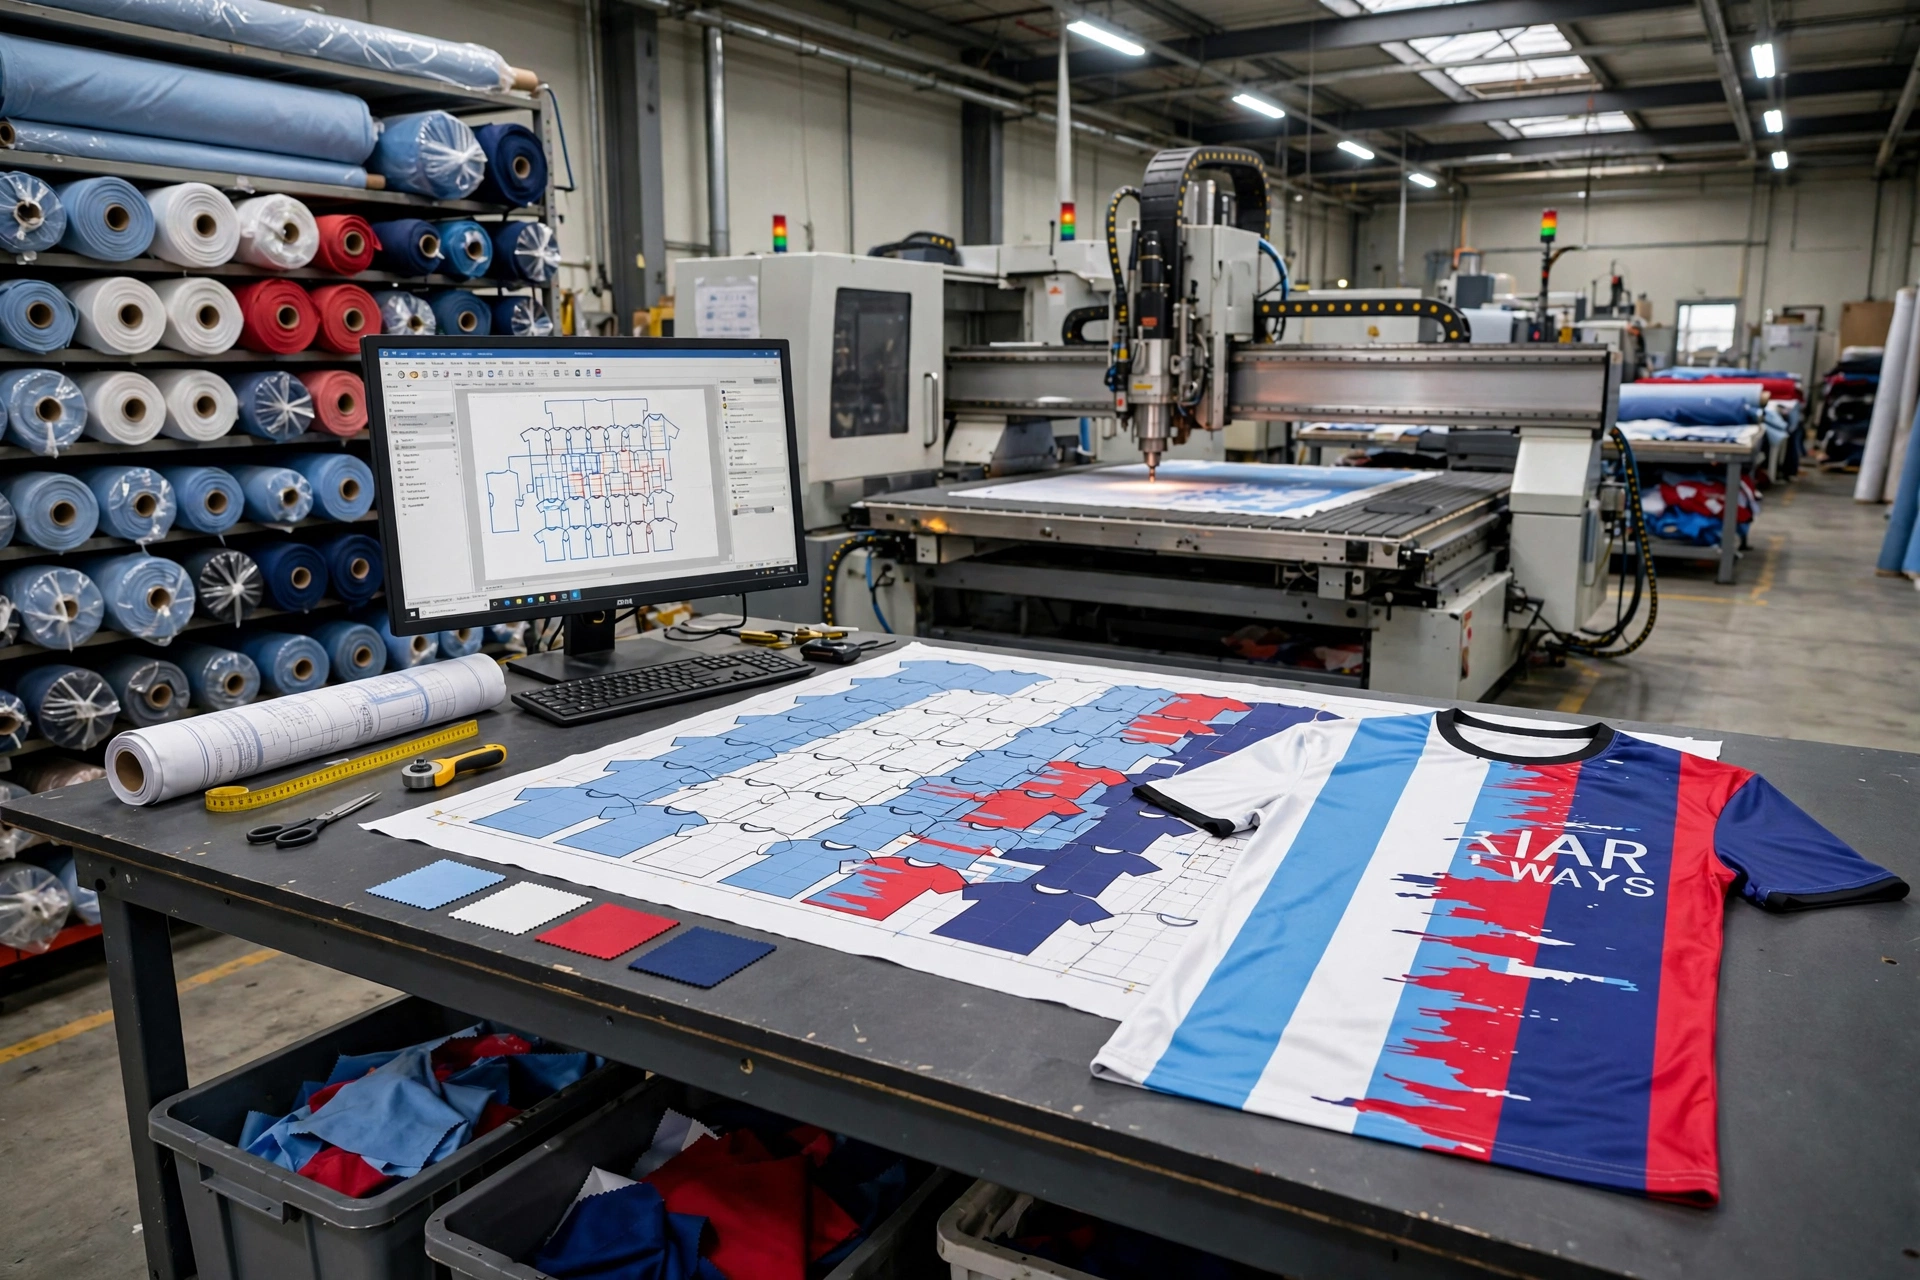
Managing large-scale production efficiently requires eliminating material waste. Our industrial cutting floors utilize advanced computer-numerical-control (CNC) nesting software to map pattern pieces across massive fabric rolls, maximizing material utilization and maintaining strict dimensional precision.
Request a quoteTo accommodate diverse commercial and institutional business models, our wholesale operations are structured around specialized production pillars:
Custom Team Uniforms and Jerseys
High-volume manufacturing of sublimated and cut-and-sew uniforms for soccer, basketball, American football, rugby, and esports leagues, featuring precise roster numbering and naming integration.
Private Label Bulk Apparel
Comprehensive wholesale production of blank or branded hoodies, tracksuits, joggers, and activewear customized with your internal woven labels, hangtags, and retail polybag packaging.
Flexible Enterprise Minimums and Tiered Pricing
While specializing in massive commercial bulk runs, we support growing brands with scalable entry thresholds, offering tiered pricing structures that reward volume growth with optimized unit costs.
We have engineered a transparent, step-by-step manufacturing workflow designed to eliminate ambiguity and streamline bulk inventory acquisition:
Specification & Volume Analysis
Submit your tech packs, bill of materials (BOM), size distribution matrices, and total volume requirements for engineering and cost evaluation.
Pre-Production Bulk Sampling
Review physical pre-production samples to verify fabric weight, stitching precision, and color calibration before authorizing full-scale bulk production.
Mass Production Execution
Upon formal sample approval, our factory initiates high-speed industrial cutting, sewing, and assembly under strict quality control supervision.
Global Logistics & Cartoning
Finished bulk inventory is securely packed into durable master cartons, labeled with precise barcoded shipping manifests, and dispatched via reliable international freight carriers.


In the competitive global apparel and institutional sports market, transitioning from mid-tier distribution to enterprise-scale inventory management requires rigorous operational discipline, advanced machinery integration, and a resilient supply chain framework. While effective branding and commercial sales strategies drive market demand, long-term enterprise profitability is anchored entirely in manufacturing consistency, predictable lead times, and optimized unit economics. Partnering with an experienced wholesale sports jerseys and uniforms manufacturer ensures that your bulk inventory meets the exacting physical standards demanded by professional leagues, educational institutions, and multinational retail chains.
When executing high-volume bulk production runs, minor oversights in dye-lot calibration, fabric tensioning, or automated cutting alignment can result in widespread inventory defects, costly shipment rejections, and damaged client relationships. Deuka Wears’s industrial manufacturing infrastructure is engineered to eliminate these operational vulnerabilities through a systematic approach to quality assurance, advanced machinery integration, and rigorous workflow management.
Request a quote
The structural superiority and visual uniformity of wholesale athletic apparel and team uniforms rely heavily on mechanized precision and standardized assembly line protocols. Unlike boutique manufacturing, high-volume bulk production requires seamless synchronization between automated computer-numerical-control (CNC) cutting tables, specialized multi-needle sewing machinery, and rigorous inline quality control checkpoints.
Request a quote
Scaling an enterprise apparel brand, managing a nationwide team uniform distribution network, or fulfilling corporate merchandising contracts requires a manufacturing partner capable of adapting fluidly to fluctuating volume demands and strict delivery deadlines. Many commercial buyers face severe operational bottlenecks when their suppliers fail to scale production capacity during peak seasonal inventory windows.
Deuka Wears’s manufacturing ecosystem is designed for structural scalability, supporting agile inventory management through a robust supply chain framework:
1
By maintaining high-capacity production floors backed by flexible minimum order frameworks, we enable enterprise clients to scale inventory quantities seamlessly from seasonal test batches to massive multi-container wholesale rollouts.
2
Every wholesale client is assigned a dedicated technical account manager who coordinates all phases of the production cycle—from raw material allocation and textile dyeing to final master carton packing and freight forwarding.
3
We manage the complexities of international trade compliance, providing accurate commercial invoices, packing lists, certificate of origin documentation, and customs clearance support to ensure smooth cross-border logistics.
Quality at scale is not a final inspection step; it is an integrated methodology embedded at every tier of our manufacturing lifecycle. Deuka Wears enforces a rigorous multi-stage quality control (QC) protocol designed to catch and rectify discrepancies before bulk shipments leave the factory floor.
Raw Material Inspection
Every incoming roll of technical fabric, fleece, elastic webbing, and thread cone undergoes rigorous lab testing for weight consistency (GSM), tensile strength, colorfastness, and shrinkage tolerance.
In-Line Cutting and Printing Verification
Pattern pieces are audited against digital tech packs for dimensional accuracy before automated CNC cutting and bulk embellishment application.
Sewing Line Supervision
Quality control technicians monitor high-speed sewing floors in real-time, verifying stitch density, seam symmetry, bar-tack reinforcement on high-stress points, and proper elastic tension.
AQL Final Pre-Shipment Audit
Finished bulk inventory undergoes rigorous final inspection utilizing international AQL (Acceptable Quality Limit) standards, verifying unit counts, barcoded polybag labeling, and durable master carton packaging.
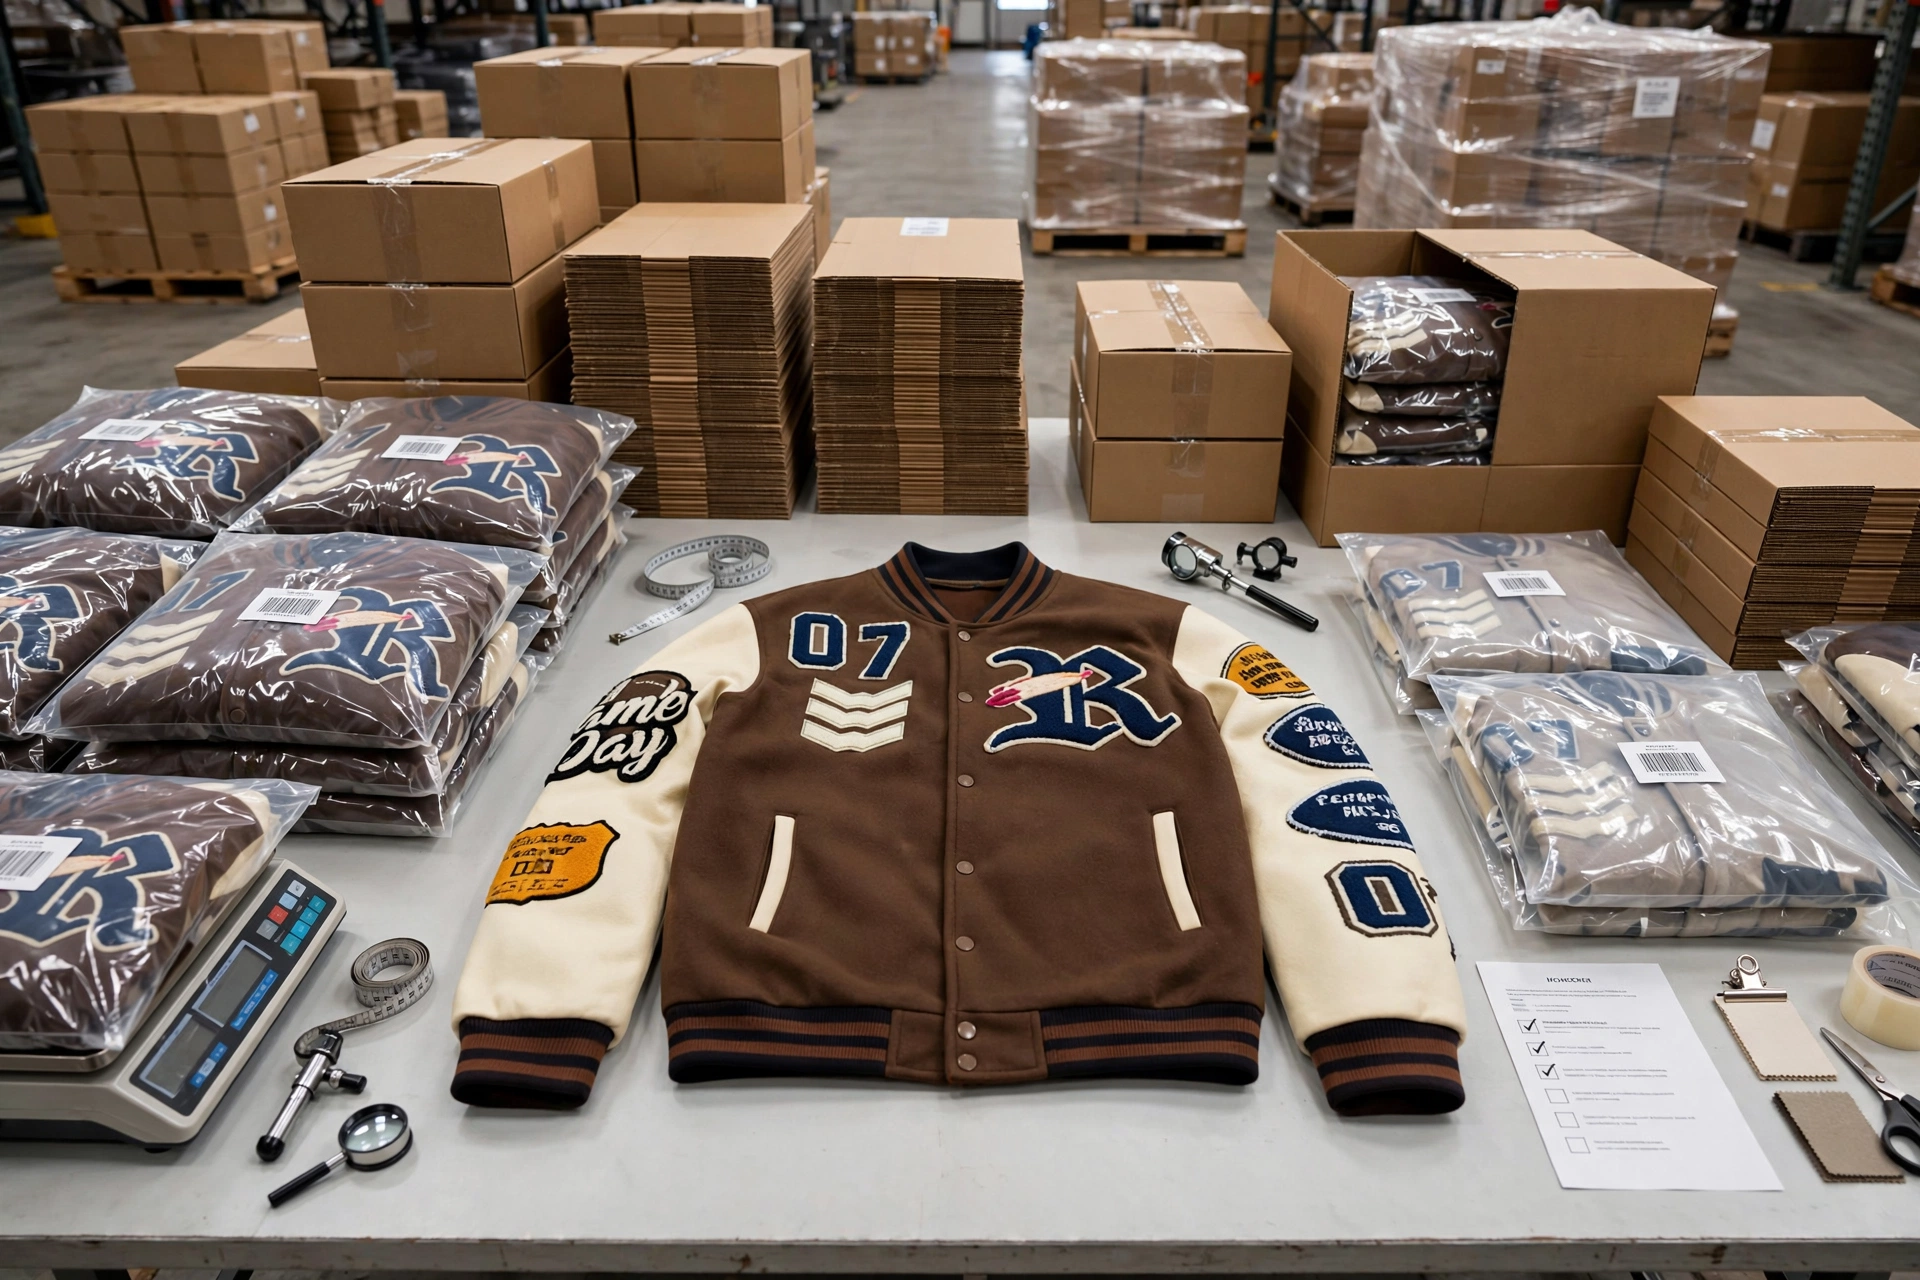
Modern institutional buyers, multinational retail chains, and conscious consumers increasingly mandate ethical supply chain transparency and environmentally responsible manufacturing practices. Deuka Wears integrates sustainability into its large-scale industrial operations without compromising product performance or cost efficiency.
Transitioning your wholesale and bulk manufacturing operations to Deuka Wears is structured to be seamless, transparent, and professionally managed. Whether you are seeking a reliable OEM partner to manufacture bespoke team uniforms or an ODM collaborator to supply a comprehensive retail activewear collection, our engineering team is prepared to execute your specifications with absolute precision.
Contact our corporate apparel division today to initiate your comprehensive tech pack review, secure your sample prototyping phase, and establish a dependable manufacturing foundation for your upcoming commercial inventory cycles.
Request a quote